Sales promises a delivery date, production finds the line is booked, and stores discovers a key material is short. When each team keeps its own records, every order turns into a round of calls and spreadsheets before anyone can give the customer a firm answer.
ERP for the manufacturing industry puts sales, purchasing, stock, production and quality on one set of records. Everyone then sees what was ordered, what is on hand and what still has to happen. This guide explains the role of a manufacturing ERP, the benefits you can test, the modules to scope and the checks to make before you commit.
The Role of ERP in a Manufacturing Business
A manufacturing ERP follows an order from first inquiry to dispatch. The quotation, the bill of materials, the purchase orders, the production run, the quality check and the invoice all point to the same order and the same item list.
That shared record is the whole point. Without it, each department answers the same question from a different source, and managers spend their time reconciling numbers instead of acting on them.
The system should follow how your plant actually runs. A make-to-order engineering shop, a batch process plant and a high-volume assembly line need different screens, different costing and different planning rules.
Benefits of ERP in Manufacturing You Can Measure
Each benefit below only holds if the underlying records are entered on time and owned by a named person. Pick the two or three that matter most and record today's baseline before you start.
Order Costs You Can Check
When material issues, labor time and purchase prices are recorded against each order, you can compare what an order was expected to cost with what it used. Agree how costs are captured first, or the reports will look precise and still be wrong.
Delivery Dates Based on Real Stock
Sales can quote a date after checking stock, open purchase orders and production load in one place. Planners still make the call, but they start from current figures rather than last week's spreadsheet.
Quality Records Tied to Batches
Inspection results, defects and test certificates link to the batch, machine or order they came from. When a customer raises a complaint, the quality team can trace the material and the run instead of searching folders.
Fewer Manual Reports
Daily production, stock and dispatch reports come straight from the system. Staff stop rebuilding the same spreadsheets each week, and managers see the same numbers the teams work from.
Better Forecasts and Purchasing
Consistent order and consumption history is the raw material for planning. Once it exists, you can add demand forecasting for manufacturers to plan materials and production runs further ahead.
Core Modules and Applications
Treat this list as a menu to scope against your own process, not a checklist to buy in full. Start with the departments involved in the problem you most need to solve.
Sales and Quotations
Contacts, leads and inquiry stages with reminders for open inquiries
Quotations built from the item master with standard rates
Sales orders that carry the specifications production needs
Inventory and Purchasing
Item master shared across every module
Purchase orders split between items you make and parts you buy in
Goods receipts that update stock without typing it twice
Reorder levels and stock by location, batch or expiry where needed
Production
A bill of materials for each product or confirmed order
Material allocation against the bill of materials, with substitutions logged
Production logs by machine, batch or shift, including downtime and issues
Quality Control
Incoming inspection before raw material is released to production
In-process and final checks recorded against the batch
Test certificates generated for each product that needs one
Shared Masters and Reports
Customer, supplier, user and item masters with clear owners
Role-based access so each team sees and changes only its own records
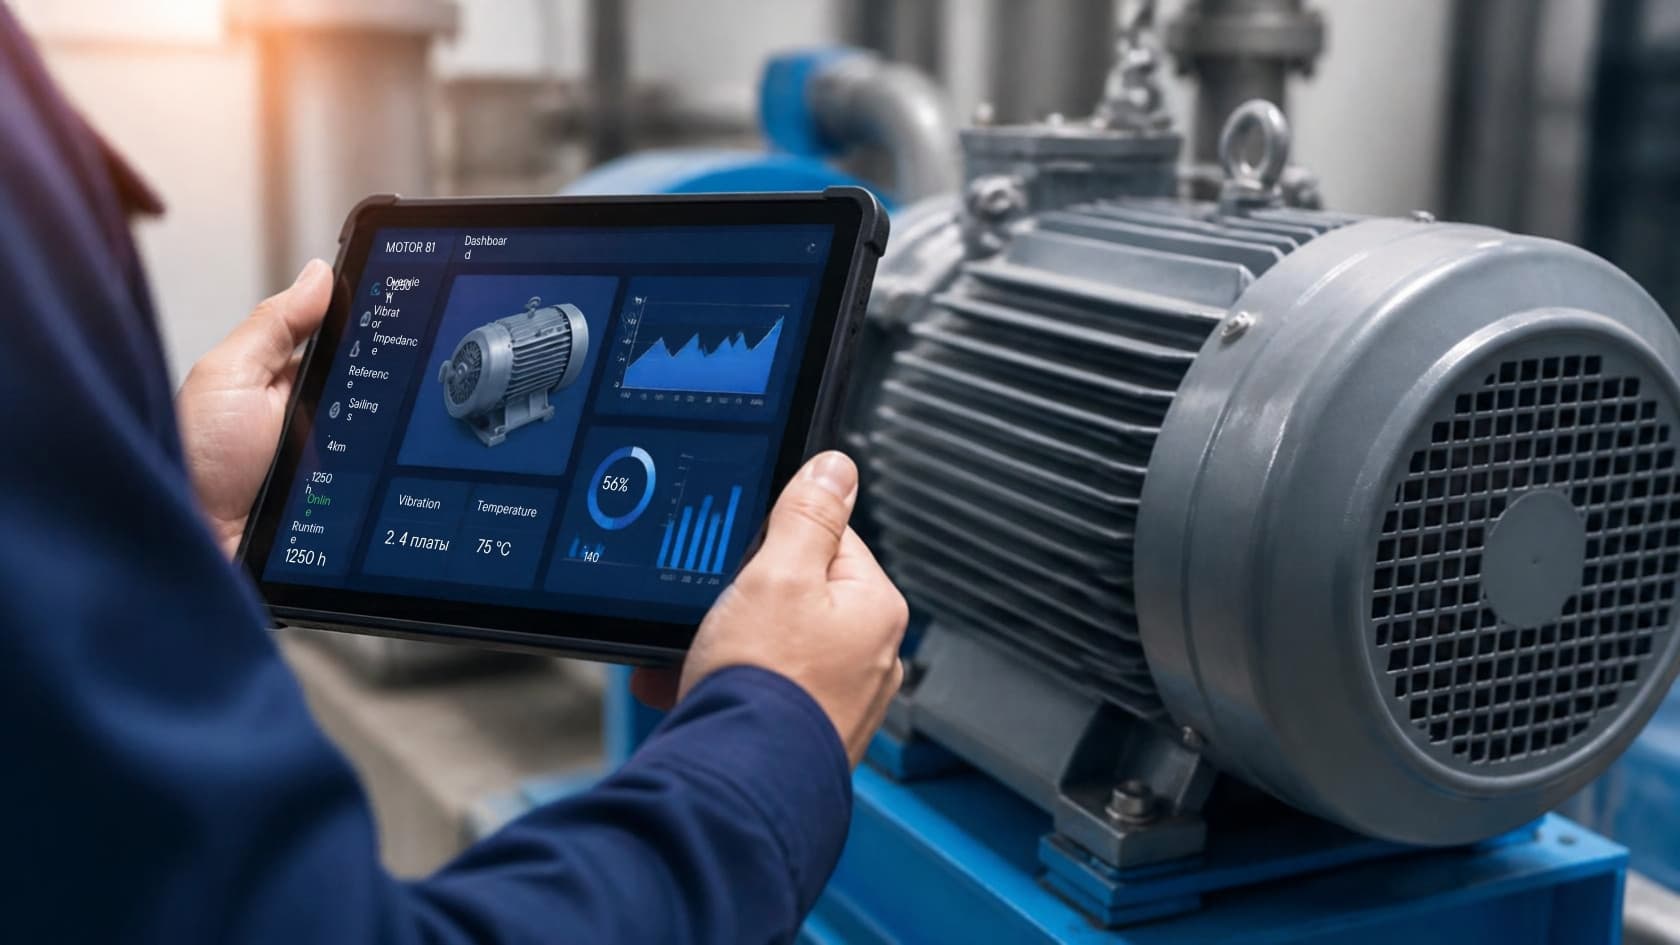
Dashboards for production, stock, cost and dispatch
Two of our projects show how these modules fit real plants. For an industrial manufacturer, quotations come from one item master, each confirmed order gets a bill of materials and allocated stock, and every product's quality check ends in a test certificate. For a colorant and plastics maker, stores and QC check each raw material receipt before use, and managers see production and cost by machine and batch.
What to Scope First
Switching on every module at once asks your team to learn everything on the same day. A staged plan lets your team learn the system on one workflow before the next one depends on it.
Find the costliest hand-off. Ask where orders, materials or reports get held up today, and who feels it.
Map the records involved. List the documents, spreadsheets and approvals in that workflow and who owns each one.
Clean the masters. Items, customers and suppliers must be accurate before anything else can be.
Set the measures. Late orders, stock shortages or rework are good tests; write down today's figures.
Run one stage live. Go live with one module or one site, fix what users report, then add the next.
Our guide to common ERP implementation mistakes covers the traps to avoid at each of these steps.
Technical Checks Before You Commit
Your technical evaluator should look past the demo. These points decide how much the system costs to run and change in year three, not just year one.
Data model: how items, variants, units of measure and bills of materials are stored, and whether your product structure fits without workarounds
Integrations: documented APIs for accounting, e-commerce, machines or shop-floor devices, and how failures are retried and reported
Migration: which history comes across, how it is cleaned and how totals are reconciled after cutover
Access and audit: role-based permissions and a log of who changed stock, prices or quality results
Performance: how screens and reports behave with several years of transactions
Ownership: who holds the source code and data, and what it costs to add a module later
Packaged ERP, Extensions or a Custom Build
A packaged ERP suits a plant whose processes match the product's standard flow. You get a faster start but accept its data model and its upgrade schedule.
When important steps do not fit, you have two options. You can extend the current system with custom modules and integrations, or you can build an ERP around your workflow, as we did for a plant whose template-based options did not match how it operated; its sales, production, inventory and quality teams now share one set of records.
Compare each option on scope, migration effort, disruption to the floor and running cost over several years, not on license price alone.
Getting Started With a Manufacturing ERP
ERP for the manufacturing industry works when it is scoped around one real problem, built on clean masters and rolled out in stages your team can absorb. Measure the change against a baseline, then add the next module.
See how we work with plants on our manufacturing industry page. If you are deciding whether to extend what you have or build something new, book a call with our founders and we will help you scope the first stage.