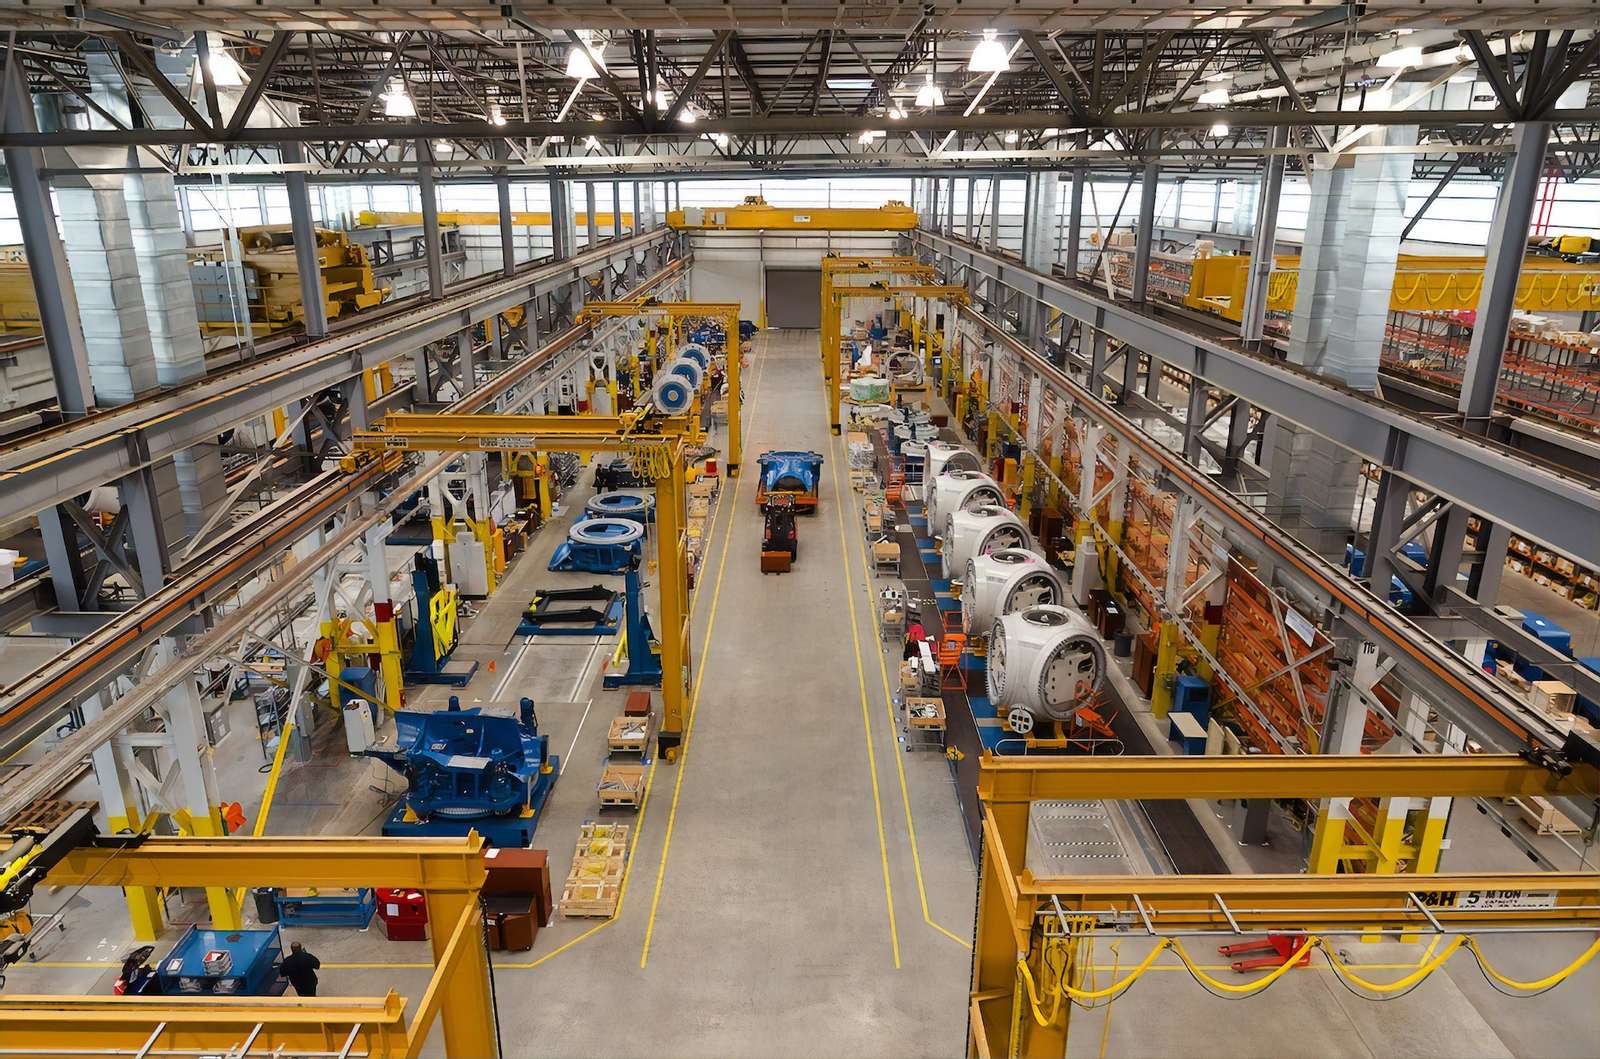
Sales confirms an order, production checks capacity, and stores checks materials. When each team uses different records, delivery promises become harder to trust.
A manufacturing ERP connects those records so teams can see what has been ordered, what is available and what still needs to happen. The value depends on the processes you connect, the quality of the data and whether people use the system consistently.
This guide explains where a manufacturing ERP can help, which modules to consider and what to check before committing to a rollout.
Role of ERP in the Manufacturing Industry
ERP gives a manufacturing business one overview of its core processes, all in one place.
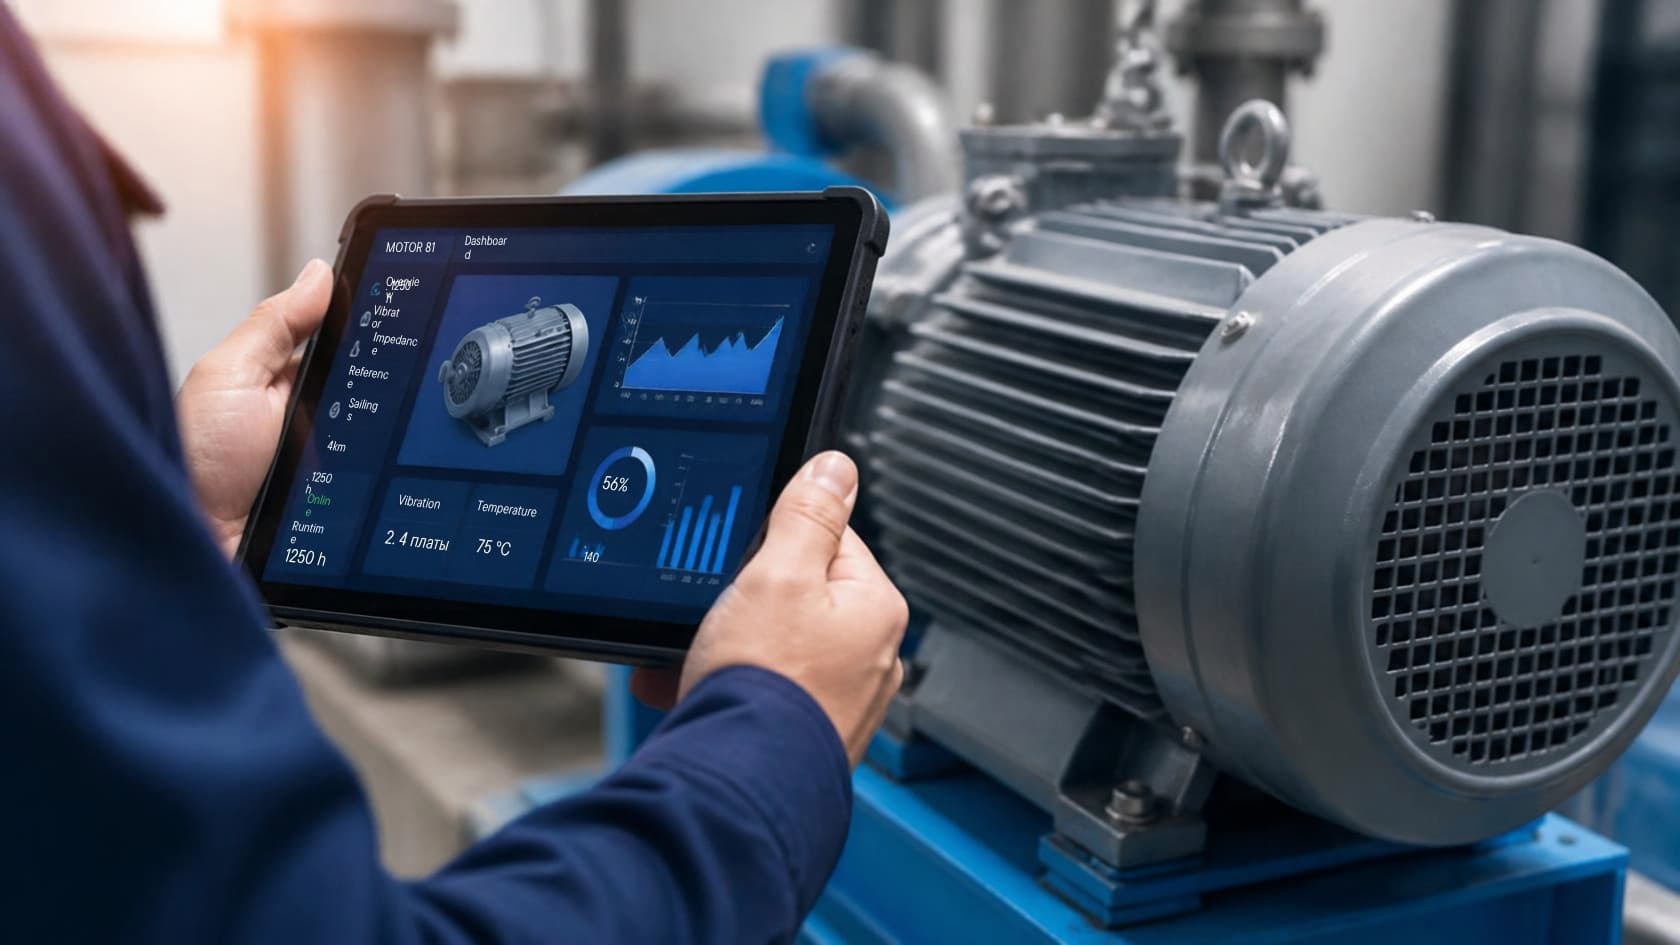
That overview follows your own process and shows real-time data on inventory management, order processing, quality checks, audit requirements, equipment setup, failures and repairs. A manufacturing unit can also track yield and metrics such as operating time, cost, efficiency and time lost.
ERP matters whether you are a small or mid-size enterprise looking to scale or a large organization streamlining its operations.
Benefits of ERP for the Manufacturing Industry
1. Understand order costs
Connect material, labor and purchasing records to compare the expected cost of an order with what it actually used. Agree how costs are recorded before relying on the reports.
2. Track the measures your team acts on
Choose measures such as late orders, stock shortages or rework. Each report should help a named person make a decision, with a way to check the underlying records.
3. Puts information in one system
Operational, performance and financial information all sit in a single system, available to the people who need it.
4. Connects the supply chain
Streamlined purchase, production, sales and distribution processes join up into a stronger supply chain.
5. Improves performance
With information available from one source, internal teams work better and customer service improves.
6. Plan capacity and material use
Use stock, equipment and production records to plan the next run. The system can make shortages and conflicts visible; planners still need to review the options.
7. Supports business forecasts
Real-time data from the ERP can be used to forecast material requirements and plan a production timeline.
8. Automates reporting
An ERP system automates many manual tasks and handles much of the reporting. Staff pull reports from the system instead of building spreadsheets by hand.
9. Trace quality checks and rework
Link inspection results and defects to the relevant batch or order. This gives the quality team a record to investigate; software alone does not assure product quality.
10. Moves information across departments
All the data is a click away, which makes it easier to act and to manage the flow of information with vendors, suppliers, stakeholders and clients.
Key Features of ERP in the Manufacturing Industry
The modules below are examples to scope against your own process. Start with the departments and records involved in the problem you need to solve.
Sales
Item Management
Contacts Management
Lead Management
Quotation Generation
Stage Tracking
Lead Activity Tracking
Periodic Reminders for Open Leads
Customer Types
Inventory
Item Master
Purchase Order
Purchase Manufacturing and Buyouts
Delivery Challan
Quality Control
Replace Materials
Service
Service Report Upload
Production
Sales Order
Bill Of Materials
Material Allocation
Replace Materials
Test Certificate
Masters
Customer Master
User Master
Item Master
Category Master
Before replacing an existing system, identify where orders, materials or reports get held up. Check whether better configuration, an integration or a custom module could resolve the gap, then compare the cost and disruption of each option.
At iTechnoSol, we study your existing business processes and work with you to build and implement custom ERP software shaped around them. Book a call with our ERP team to get started.